3D CNC beam drilling machine: throughput, hard materials, tooling cost and defects explained
- Share
- Issue Time
- Oct 27,2026

How many holes can a 3D CNC beam drilling machine actually drill per shift?
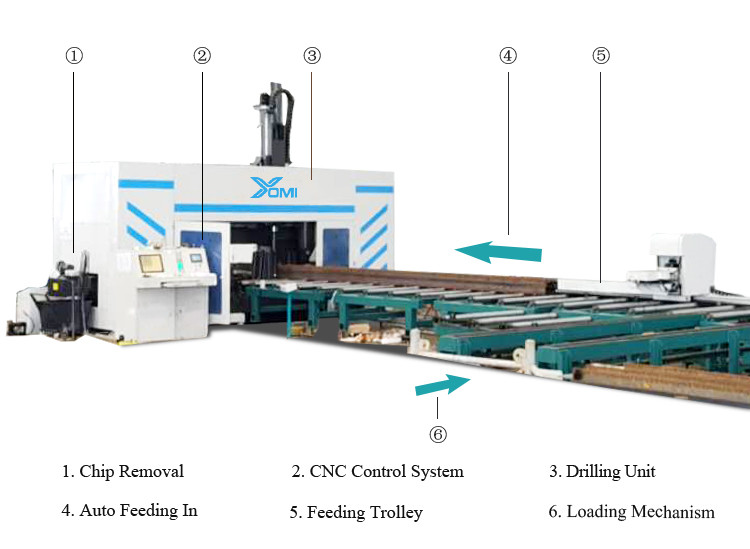
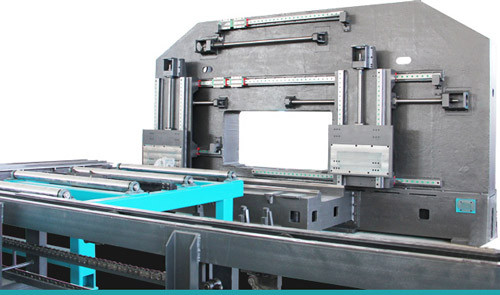
The YM-3D1250 drills at 2-4 seconds per hole with three BT40 spindles (3 x 15 kW) working the web and both flanges simultaneously, so a dense connection-plate pattern on one beam position is finished in a single pass instead of three re-clamped setups. In practice a beam with 100-200 holes takes roughly 8-20 minutes including servo feeding at up to 20 m/min and hydraulic clamping, which translates to 20-40 beams per 8-hour shift depending on hole count and profile size. The real bottleneck is rarely the spindle: it is crane loading of 10 t beams, first-article checks on new profile sizes, and emptying the chip trolley. Plan your material handling for those, not for spindle speed.
Can a CNC beam drilling machine drill stainless steel and high-strength steel?
Yes, cold drilling handles any material the tooling can cut, including Q355/Q420 high-strength steels and stainless steel, because there is no thermal distortion like plasma or flame hole cutting. The parameters change, not the machine: carbon steel drills comfortably at 80-100 m/min surface speed with coated carbide, 4140-type alloy steel drops to about 80 m/min, and 316 stainless needs 40-50 m/min with a heavier feed to avoid work hardening. For stainless, keep feed constant rather than dwell, use mist cooling generously, and expect 30-40% shorter tool life than carbon steel. The 30-3000 r/min spindle range on the YM-3D1250 covers all of these speed windows for holes from 8 to 40 mm.
What does a drilled hole really cost in drill bits and tooling?
Tooling is the highest-wear consumable on a beam drill line, so budget it per hole rather than per month. Coated HSS drills are cheap per piece but run 25-35 m/min; carbide-tipped or indexable drills cost 3-5 times more but run 80-150 m/min and last far longer between regrinds, which earns their price on repeated bolt-hole patterns. Expect 300-800 holes per sharpening depending on flange hardness, with BT40 holders re-touched after every tool change. A practical rule for budgeting: tooling plus mist fluid typically runs 2-4% of machine price per year at one-shift operation. Keep a stocked set of the diameters that appear most in your drawings - reordering a drill mid-shift is the classic cause of unplanned downtime.
Why do drilled holes come out oversized, bell-mouthed or with broken drills?
Three different causes, three different fixes. Hole walking (0.3-0.8 mm offset) happens when the drill tip skates on mill scale at first contact - spot-face or reduce the approach feed so the flutes bite before the hole wanders. Bell-mouthed holes on thin 6 mm webs happen when the web flexes under thrust instead of cutting - lower feed to 0.08-0.10 mm/rev and use peck drilling in 1xD increments so chips clear instead of packing. Broken drills almost always show blue chips first: that is heat from a dull edge or excessive feed, and the next twenty holes will come out oversize if you keep running. Inspect drills on a fixed hole-count schedule rather than waiting for a breakage.
Is mist cooling enough, or do I need through-spindle coolant for deep holes?
The YM-3D1250 uses mist (minimum quantity lubrication) through 3 spray nozzles at 0.5 MPa compressed air, which is the standard setup for beam lines: drills stay cool, beams exit nearly dry for downstream marking and welding, and there is no flood coolant disposal cost. Mist reaches the drill tip fine on holes up to roughly 3xD depth on flanges, where gravity also helps chip evacuation. For the deepest holes on a vertical flange face, the control runs an automatic peck cycle that retracts to clear the flutes - that matters more than coolant type on a horizontal web, which traps swarf against the drill shank. If your drawings routinely need deep, large-diameter holes, tell the supplier at quotation stage so the peck parameters are pre-loaded per material.
Can it drill box beams, channels and angle steel, or only H beams?
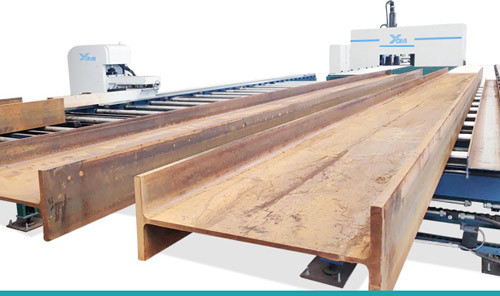
The YM-3D1250 handles more than just H beams. Within its 1250 mm workpiece width it drills H beams from 150 x 80 to 1250 x 600 mm, U channels and box beams up to 1250 x 400 mm, and angle steel up to 200 x 200 x 16 mm, with material thickness up to 80 mm. What changes between profiles is the clamping and support configuration - box beams need internal roller support positions and angles sit differently in the roller frames. Workpiece lengths run from 3,000 mm short material (processed automatically) up to 12 or 15 m. If your mix includes irregular profiles, send the profile drawings and hole positions at inquiry stage so the clamping setup is confirmed before you order.
Can it replace our manual radial drill team, and how does the workflow change?
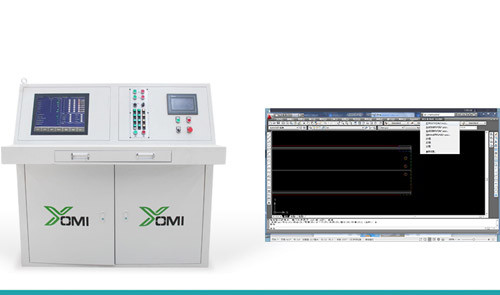
Yes, and the workflow change is bigger than the speed gain. A radial drill needs manual measuring, scribing, and one face per setup with re-clamping between faces; the CNC line reads the TEKLA DSTV file exported by your detailing software, generates the program with a 3D preview of every hole, and drills all three faces in one pass - no manual layout at all. Staffing drops from a layout man plus drill operators to one supervisor per shift; programming moves to the office where the model already exists. Because drilling is cold processing, hole geometry carries no heat distortion, and 0.5 mm accuracy within a hole group means bolted connections line up on site without reaming. The reskilling is modest: operators learn file import, clamping profiles, and first-article checks in a few days, since no G-code writing is required.
How does the machine handle beam length measurement and short offcuts?
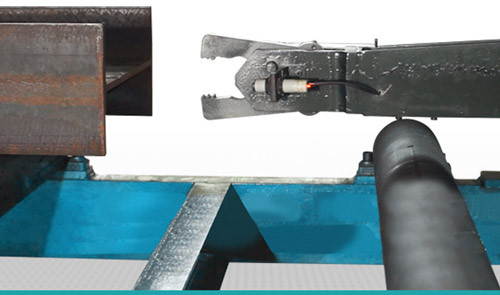
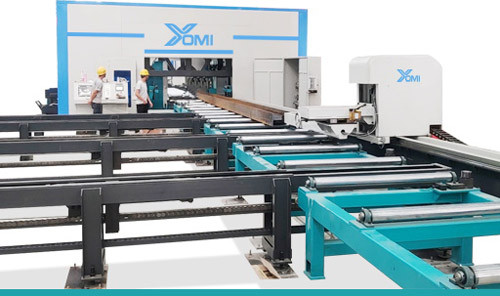
The feeding system is a 5 kW servo trolley that carries beams up to 10 t (at 1 t/m) along the roller table at up to 20 m/min, with the CNC controlling infeed positioning axis speeds of 0-12 m/min so the beam stops precisely under the drilling heads. Raw material up to 12,000 mm (12 or 15 m configurable) is processed without repositioning because the complete line is about 32 m long: a 14 m feed conveyor, the 2 m drilling unit, and an outfeed section with finished-piece storage. Short offcuts matter too - material from 3,000 mm is processed automatically, so you are not hand-carrying stubs to a radial drill. That short-material capability plus repeatable laser positioning is what lets fabricators buy full-length stock and nest beams without a remnant pile of unusable ends.
Technical Specifications of 3D CNC Beam Drilling Machine
| Parameter | Value |
|---|---|
| Share | |
| Categories | 3D Beam Drilling Machine |
| Brand | YOMI CNC Cutting&Welding Machinery |
| Product Specifications | YM-3D1250 |
| Beam web height | 200-1250mm |
| Max drilling thickness | ≤80mm |
| Max drilling hole diameter | ¢40mm |
| Spindle motor power | 3x15KW |
| Effective feeding length | 12m |
| Maximum feeding speed | 20m/min |
| Positioning CNC axis moving speed | 10~6000mm/min |
| Feeding CNC axis moving speed | 10~12000mm/min |
| Model | YM-3D1250 |
| Workpiece | H beam, U beam, box beam, angle steel |
| Maximum workpiece width | 1250 mm |
| Drilling diameter | 8 to 40 mm |
| Spindle | BT40 taper, convertible to M4, 30 to 3000 r/min |
| Spindle motor power | 3 x 15 kW |
| CNC axes | 7 |
| Hole accuracy | 0.5 mm within a hole group under 640 mm; 1.0 mm per 10,000 mm between groups |
| Feeding | 10 t capacity at up to 20 m/min |
| Main host size and weight | About 5600 x 1600 x 3400 mm, about 20,000 kg |
| Item | Parameter |
| H beam | 150 x 80 to 1250 x 600 mm |
| U beam | 150 x 80 to 1250 x 400 mm |
| Box beam | 150 x 80 to 1250 x 400 mm |
| Angle steel | 200 x 200 x 16 mm |
| Thickness | 80 mm or less |
| Length | 12 or 15 m, or customized |
| Short material limit | Automatic processing from 3,000 mm |
| Drilling power boxes | 3 pcs |
| Drilling hole diameter | 8 to 40 mm |
| Spindle speed | 30 to 3000 r/min |
| Spindle taper hole | BT40, convertible to M4 |
| Spindle motor power | 3 x 15 kW |
| CNC axis quantity | 7 pcs |
| Fixed, moving and intermediate shaft servo power | 3 x 2 kW |
| Positioning CNC axis speed | 0 to 10 m/min |
| Feed CNC axis speed | 0 to 5 m/min |
| Machined hole accuracy | Adjacent holes in a group under 640 mm: 0.5 mm; adjacent hole group distance: 1.0 mm per 10,000 mm |
| Feeding trolley servo motor power | 5 kW |
| Maximum feeding speed | 20 m/min |
| Maximum feeding weight | 10 t at 1 t/m |
| Maximum width of workpiece | 1250 mm |
| Mist cooling nozzles | 3 pcs at 0.5 MPa compressed air |
| Main host dimension, L x W x H | About 5600 x 1600 x 3400 mm |
| Main host weight | About 20,000 kg |
| Item | Traditional radial drilling, YOMI YM-3D1250 |
| Layout and marking | Manual measuring and scribing, Automatic from the TEKLA DSTV model |
| Faces per setup | One face, re-clamped for each face, Three faces in one pass |
| Hole accuracy | Depends on operator skill, 0.5 mm within a hole group |
| Consistency | Varies by shift and operator, Program driven and repeatable |
| Throughput | Low, with multiple handling steps, Continuous roller-table flow at up to 20 m/min |
Product Gallery

Applications
The 3D CNC Beam Drilling Machine is widely applied in steel structure prefabricated buildings, bridge and infrastructure construction, shipbuilding and marine engineering, heavy machinery manufacturing, power plant and industrial facilities, and offshore wind power structures.
Learn more about the 3D CNC Beam Drilling Machine:
https://www.steelstructurer.com/pid18376284/3D-CNC-Beam-Drilling-Machine.htm
For more information about 3D CNC Beam Drilling Machine and other steel structure intelligent equipment, contact YOMI CNC Cutting & Welding Machinery. Our team of experts is ready to help you find the best solution for your manufacturing needs.